Why the Coating Is Where Suppliers Cut Corners
“Galvanized” is the most abused word in hanger strap buying. Two galvanized hanger straps can look identical on a warehouse shelf yet differ by half in zinc thickness — and the difference appears two years later as rust streaks on a customer’s ductwork. Zinc is one of the largest cost components of the product, so an under-specified or under-inspected coating is also the most common place a supplier quietly saves money. This galvanized hanger strap coating inspection guide explains how to write coating requirements into your purchase order, which documents to demand, and which tests actually verify the zinc at receiving — based on 16 years of manufacturing galvanized strapping at our Jiangmen facility.
What “Galvanized” Means on a Hanger Strap
Hanger straps are made from pre-galvanized steel strip: the coil is continuously hot-dip galvanized at the mill before slitting and punching. The governing standard is ASTM A653, and the coating weight is stated as G30, G60, or G90 — the total zinc on both sides in ounces per square foot: 0.30, 0.60, and 0.90 oz/ft². Converted to the units your suppliers may quote: G90 equals roughly 275 g/m² total, about 19 µm per side; G60 is about 183 g/m², 13 µm per side; G30 is about 92 g/m², 6.4 µm per side. A purchase order that says only “galvanized” specifies nothing, because all three are galvanized and all three cost differently. In our quoting experience, vague wording is the single most reliable predictor of a later coating dispute — the invoice always lands on the cheapest interpretation.
How to Specify Coating in the Purchase Order
A defensible coating clause needs six elements. First, the designation with a minimum: “G60 minimum, ASTM A653” — never a bare nominal. Second, the verification standard: ASTM A90 for the weigh-strip-weigh reference method and ASTM A239 for the Preece test. Third, sampling: ISO 2859-1 at AQL 1.0 for critical defects, with the number of rolls to test written into the order. Fourth, surface defects: maximum bare spot size and count per roll, and edge condition. Fifth, white rust: define what is acceptable after ocean transport — typically light, removable haze only, no pitting. Sixth, remedies: replacement, rework, or price adjustment for nonconforming lots, plus certificate requirements. The clause does not need to be long; one paragraph covering these six points, referenced in the specification sheet, converts a coating argument into a measurable claim.
Documents to Demand Before Shipment
Ask for documents that contain measurements, not reassurances. The mill certificate for each lot should list the actual coating weight test results per heat and coil, not merely the words “conforms to G60.” Look for the test method used, the measured values, and the date. Batch traceability matters: the certificate, the coil tags, and the packing list should carry the same lot numbers, so a failed coil can be traced to its certificate in minutes. Finally, request pre-shipment photographs of the coating gauge being applied to your coils before packing. A supplier that measures and photographs its coating before shipping is showing you the same discipline it used in production; one that will not is telling you something too.
Acceptance Tests That Actually Verify Zinc
At receiving, work from non-destructive to destructive. Start with visual inspection under good light: the coating must be uniform, free of bare spots, heavy dross lines, and ash inclusions, with edges fully covered — sheared edges are always the first place rust starts. Then measure with a magnetic thickness gauge per ISO 2178: take five to ten readings across both sides of several rolls and record both the average and the minimum, because the minimum is what fails in service. For a binding result, use the weigh-strip-weigh method of ASTM A90: cut a sample, weigh it, strip the zinc in inhibited hydrochloric acid, weigh again, and divide the weight loss in ounces by the sample area in square feet. A 2 in × 2 in sample that loses 0.011 oz of zinc has lost about 0.40 oz/ft² — compare that against your ordered coating class. The Preece copper sulfate test of ASTM A239 offers a quicker pass-or-fail screen: the coating survives a specified number of one-minute dips, with more dips required for heavier classes. Finally, bend a sample 180 degrees around a rod sized to the strip thickness; a sound coating flexes without flaking. Salt spray hours per ASTM B117 are useful for qualifying a supplier, not for accepting a lot — a 24-hour test cannot predict five years of roof exposure, so do not let a salt spray certificate substitute for gauge readings.
White Rust, Disputes, and Rework
White rust is zinc’s own corrosion product, formed when moisture is trapped between coil wraps during storage or sea transport. It is not automatically a defect: a light, powdery haze that wipes away with a dry cloth is cosmetic, while heavy white rust with pitting means the zinc is partly consumed and the base steel is at risk. If a lot fails, isolate it, photograph the evidence with the lot tags visible, and keep samples and records for at least twelve months. Reasonable outcomes include replacement, a negotiated price adjustment for reduced service life, or return — re-galvanizing finished strap is rarely economical. For outdoor or coastal projects, remember that no inspection can upgrade a G30 coating into a G90: if the destination environment is aggressive, specify stainless or a heavier coating from the start, as covered in our galvanized vs. stainless steel strapping comparison.
Don’t Forget the Hole Edges
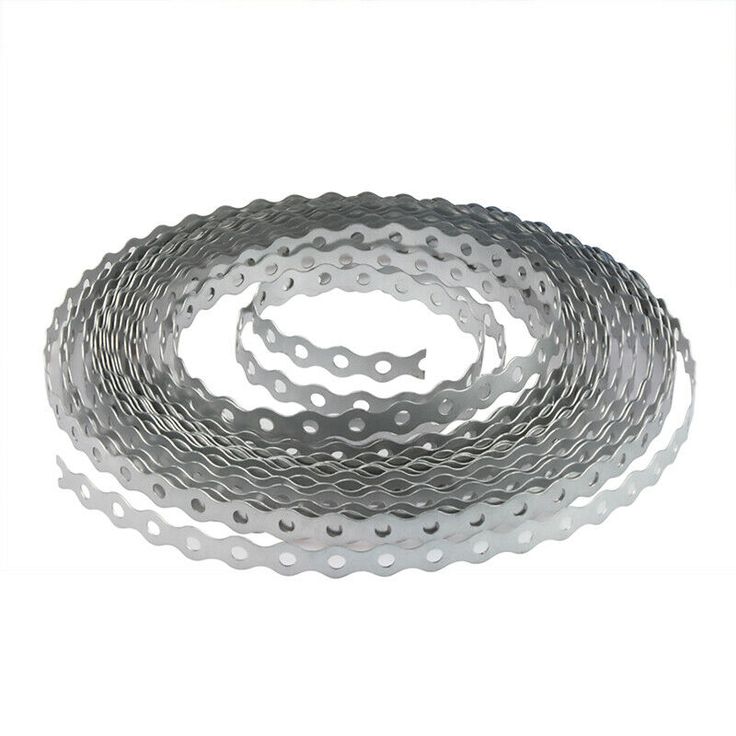
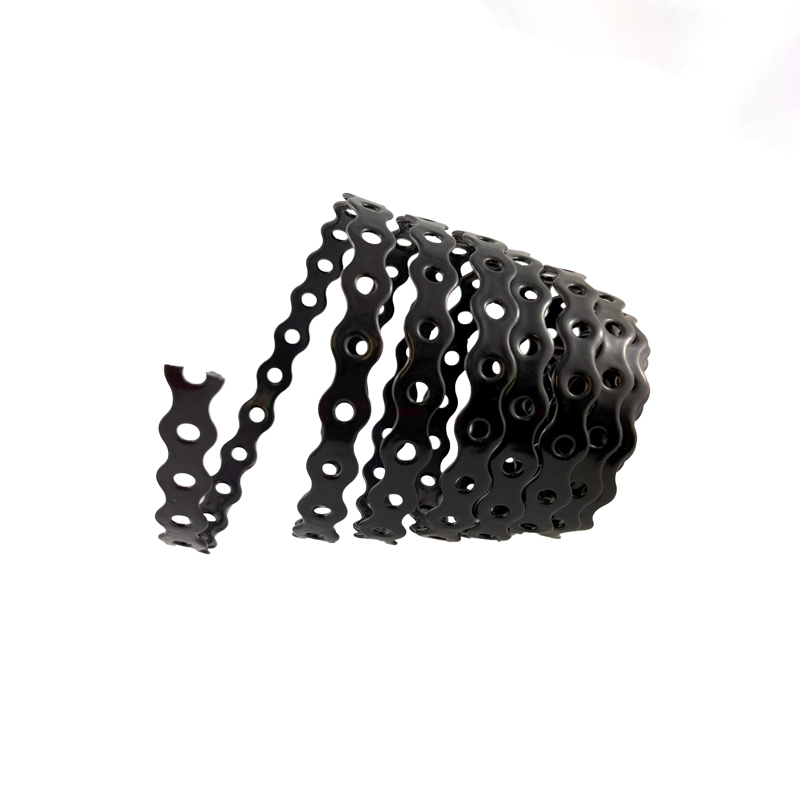
Here is a detail most buyers miss, and we mention it because it shows up in warranty claims: perforated strap is punched after galvanizing, so the walls of every hole are bare steel, not zinc. The fastener sits in that hole, moisture collects there, and rust starts exactly where the load is. On indoor dry projects this is cosmetic; on anything wet, specify one of three remedies in the order — a zinc-rich touch-up applied to hole walls at the factory, electrogalvanizing applied after punching, or stainless steel for the whole product. If your supplier cannot answer what they do about hole-wall protection, that is your answer: nothing. This single clause is worth more in service life than the difference between two coating classes.
One-Page Coating Acceptance Checklist
- PO states coating class with “minimum”: G30, G60, or G90 per ASTM A653
- Verification methods named: ASTM A90 weigh-strip-weigh, ASTM A239 Preece, ISO 2178 magnetic gauge
- Sampling plan written in: ISO 2859-1, AQL 1.0 for critical defects
- Mill certificate shows measured coating values and lot numbers, not just “conforms”
- Coil tags, certificates, and packing list share the same traceability numbers
- Visual check: uniform zinc, no bare spots, edges covered
- Gauge readings recorded: average and minimum per roll, both sides
- Bend test passed without flaking
- White rust: light haze acceptable, pitting rejected
- Failed lots isolated, photographed, and escalated with samples retained
Conclusion
Coating is invisible insurance: you cannot see the difference between G30 and G90 on the day the goods arrive, which is exactly why it must be specified, documented, and measured instead of assumed. This galvanized hanger strap coating inspection checklist turns zinc thickness from a matter of trust into a number on a gauge. For more on choosing and vetting suppliers, see our steel strapping supplier guide, download current product catalogs, or request coating test reports and samples through the contact page.